
Print Schedule
Hold: do not print flight parts (Ryan, 2026-10-10). The beds below are the first build, Fuselage C v2.4B (Ryan, 2026-10-13), from
tools/slice_all.py --fusC. They do not print until Ryan releases the hold, except bed g21 (avionics), which Ryan released on 2026-10-18, and bed g19 (the keel B and stilt B soles), released on 2026-10-19. Bench tools and test prints are exempt: they are not airframe parts, so they can print now (Ryan, 2026-10-11).
This page gives the fastest order to print the first build. The build is Fuselage C v2.4B with the own-section wing and its fences, keel B, the lights and the blank payload cover. Twenty-two beds print on the Core One+. The elevons (g08) print on the Kobra Max at the same time: standing, they are 275.5 mm tall, more than the Core One+’s 270 mm. Parts that have identical settings go on one bed. The Core One+ bed order is the provable optimum for the times when a person is available to clear the bed (tools/plan_schedule.py).
| Availability | First build | With 15 % added |
|---|---|---|
| Home all day (7:00 to 23:00) | 4.9 days | 5.6 days |
| Workdays (7:00 to 8:00, 17:00 to 23:00) | 6.1 days | 6.7 days |
The 15 % covers estimates that are too short or one reprint. The 23 beds take 119.6 hours and 1,153 g of filament in total (slicing/summary-fusC.txt); the Core One+ beds are 112.0 hours of that. Before day 1, dry the PLA Aero for 8 hours, then print the Dowel Coupon (47 minutes) to set the dowel hole size.
The 23 beds
Section titled “The 23 beds”The files are slicing/gcode/fusC/g*.bgcode, except g08, which is g08-lw-Elevons.gcode for the Kobra Max. The related .3mf projects are in slicing/projects/fusC/. Each bed has a page in Print jobs, with its parts, settings and a plan of the bed.
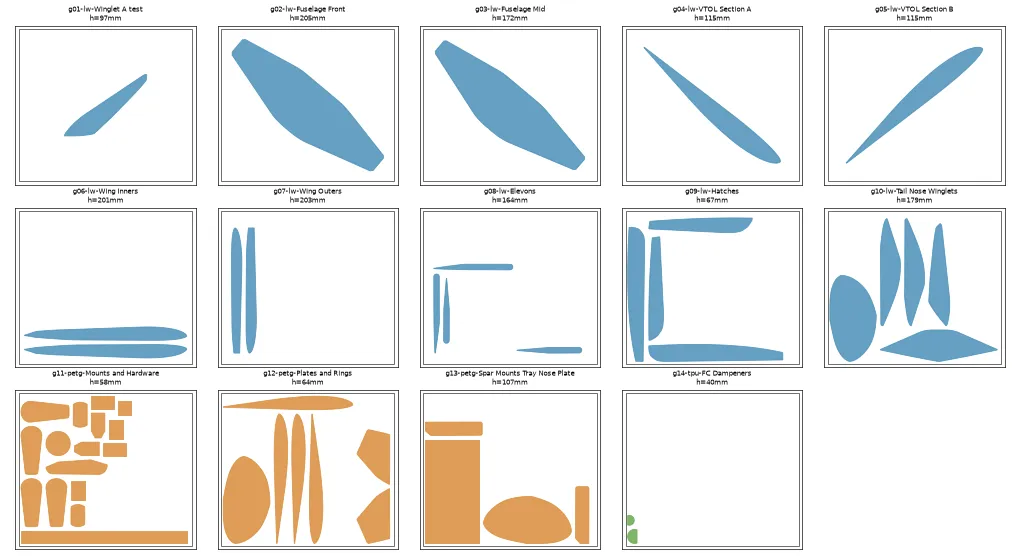
| Bed | Parts | Material | Time | Filament |
|---|---|---|---|---|
| g01 | Wing Tip (own section) | PLA Aero | 1.3 h | 7.8 g |
| g02 | Front | PLA Aero | 12.6 h | 83.7 g |
| g03 | Bay | PLA Aero | 12.1 h | 80.0 g |
| g04 | VTOL Section (port) | PLA Aero | 6.0 h | 40.7 g |
| g05 | VTOL Section (starboard) | PLA Aero | 5.9 h | 40.7 g |
| g06 | Wing Inner (own section), Wing Inner (own section) (starboard) | PLA Aero | 11.9 h | 79.4 g |
| g07 | Wing Outer (own section), Wing Outer (own section) (starboard) | PLA Aero | 6.3 h | 43.7 g |
| g08 | Kobra Max. Elevon (own section), Elevon (own section) (starboard) | PLA Aero | 7.6 h | 28.3 g |
| g09 | Hatch | PLA Aero | 4.3 h | 31.3 g |
| g10 | Tail, Nose Cone (ours), Wing Tip (own section) (starboard) | PLA Aero | 4.2 h | 28.4 g |
| g11 | Pusher Motor Mount (ours), Wing Clip x2 (ours), Landing Light Frame, Strobe Plate, Strobe Ring (top) on its print foot, Strobe Dome Buck. One plate since 2026-10-19 in place of g11 and g22 (Ryan), so it warms up once | PETG | 2.9 h | 55.4 g |
| g12 | Nose Cone Plate (ours), Nose Ring Plate, VTOL Section Plate (PETG) (port), VTOL Section Plate (PETG) (starboard), Wing Inner Plate (ours), Wing Inner Plate (ours) (starboard), Wing Fence (own section, X 445), Wing Fence (own section, X 445) (starboard) | PETG | 1.3 h | 31.4 g |
| g13 | Battery Tray B (slide), VTOL Spar Mount (PETG) (port), VTOL Spar Mount (PETG) (starboard) | PETG | 4.0 h | 89.4 g |
| g14 | Antenna Slot Grommet (port), Antenna Slot Grommet (starboard), Pusher Lead Grommet (TPU), Wire Window Cover (port), Wire Window Cover (starboard), Light Battery Saddle (TPU) (C v2.4B, aft 8, lead forward), Conduit Seal (C) (port), Conduit Seal (C) (starboard), Lucid Edge Gaskets (TPU) [print flat] | TPU | 0.8 h | 8.1 g |
| g15 | Charge Power Bracket, Camera Arm, Radio Cradle Base (XIAO, nose), Canopy (PETG), Beacon Carrier (PETG) | PETG | 3.0 h | 62.4 g |
| g16 | Airspeed Nose Bracket, Radio Cradle Lid (XIAO), CG Slider (port), CG Slider (starboard), CG Slider Pinion, SMA Bulkhead Bracket (J2 single, port wall, split), Power Hub Pad (port wall), LoRa A Coax Clip (rise, port wall), LoRa B Park Saddle, Trim Bracket, Radio Pigtail Clip (port wall), SMA Bulkhead Bracket (ELRS, Spar Box) (port), SMA Bulkhead Bracket (ELRS, Spar Box) (starboard), RP4TD Pigtail Tie Bar (Bay) (port), RP4TD Pigtail Tie Bar (Bay) (starboard), Static Line Clip (starboard wall), Servo Mount MD65MG (own wing), Servo Mount MD65MG (own wing) (starboard), M10 Hanger, Hatch Catch (PETG), Lights Node Seat Pad (C v2.4B, forward), Lights Node Seat Pad (C v2.4B, aft) | PETG | 3.6 h | 75.9 g |
| g20 | Spar Box | PLA Aero | 7.1 h | 47.8 g |
| g21 | Avionics Plate (LUX F765), Q43 Seat, Lucid Edge Bracket (PETG), Lucid Caps Cradle (PETG), Lucid Caps Cradle B (PETG), Deck Pad (PETG) (port), Deck Pad (PETG) (starboard), Rim Frame (PETG) (port), Rim Frame (PETG) (starboard), Aria Tray (PETG) | PETG | 3.0 h | 51.8 g |
| g24 | Payload Cover (blank), on its print foot with two snap-off waist fins and organic supports inside. In ASA since 2026-10-21 (Ryan): load ASA for this bed (265 C, 110 C bed; it waits for a 40 C chamber) | ASA | 3.1 h | 47.1 g |
| g23 | Position Light Window (tail), Position Light Window (tip) (own section), Position Light Window (tip) (own section) (starboard), Strobe Clip Ring | PETG | 0.1 h | 1.6 g |
| g17 | Keel B Mount (cable riser), Keel B Mount (cable riser) (starboard), Front Stilt B Mount (bolt pilot) x2 | PETG | 8.2 h | 131.4 g |
| g18 | Keel B Blade (antenna bay) x2, Front Stilt B Blade (cored), Front Stilt B Blade (cored) (starboard), Antenna Cassette Lid (keel B), Antenna Cassette Lid (keel B) (starboard) | PLA Aero | 8.8 h | 59.1 g |
| g19 | Keel B Sole (bead boss) x2, Front Stilt B Sole x2 | PETG | 1.4 h | 27.4 g |
Each VTOL Section needs the diagonal of the bed, so the two VTOL Sections cannot share a bed. Parts on one bed also print in less time: the printer does the heat-up, homing and first-layer setup only one time for each bed.
Home all day
Section titled “Home all day”| Start | Bed | Hours | Ends |
|---|---|---|---|
| Day 1 07:00 | g01 Wing Tip A (own section) | 1.3 | 08:20 |
| Day 1 08:35 | g05 C VTOL Section (starboard) | 5.9 | 14:28 |
| Day 1 14:43 | g10 C Tail Nose Cone Wing Tip B | 4.2 | 18:58 |
| Day 1 19:13 | g24 g24-asa-C Payload Cover (blank) | 3.1 | 22:16 |
| Day 1 22:31 | g17 Keel B and Stilt B Mounts | 8.2 | Day 2 06:45 |
| Day 2 07:00 | g16 Servo Airspeed Radio Holders and Slider | 3.6 | 10:37 |
| Day 2 10:52 | g04 C VTOL Section (port) | 6.0 | 16:49 |
| Day 2 17:04 | g13 C Spar Mounts and Slide Tray | 4.0 | 21:03 |
| Day 2 21:18 | g06 Wing Inners (own section) | 11.9 | Day 3 09:14 |
| Day 3 09:29 | g21 C Avionics Q43 Lucid and Aria | 3.0 | 12:29 |
| Day 3 12:44 | g07 Wing Outers (own section) | 6.3 | 19:03 |
| Day 3 19:18 | g03 C Bay | 12.1 | Day 4 07:25 |
| Day 4 07:40 | g09 C Hatch | 4.3 | 12:00 |
| Day 4 12:15 | g11 Mounts Hardware and Lights | 2.9 | 15:09 |
| Day 4 15:24 | g12 Plates and Fences | 1.3 | 16:44 |
| Day 4 16:59 | g15 C Canopy Beacon Carrier Charge Camera Arm | 3.0 | 20:00 |
| Day 4 20:15 | g02 C Front | 12.6 | Day 5 08:53 |
| Day 5 09:08 | g14 Seals | 0.8 | 09:54 |
| Day 5 10:09 | g20 C Spar Box | 7.1 | 17:15 |
| Day 5 17:30 | g23 Clear Light Windows | 0.1 | 17:36 |
| Day 5 17:51 | g19 Keel B and Stilt B Soles | 1.4 | 19:12 |
| Day 5 19:27 | g18 Keel B and Stilt B Blades and Lids | 8.8 | Day 6 04:17 |
At the same time, the Kobra Max prints g08 Elevons from Day 1 07:00 to 14:36.
Workdays
Section titled “Workdays”| Start | Bed | Hours | Ends |
|---|---|---|---|
| Day 1 07:00 | g01 Wing Tip A (own section) | 1.3 | 08:20 |
| Day 1 17:00 | g13 C Spar Mounts and Slide Tray | 4.0 | 20:58 |
| Day 1 21:13 | g19 Keel B and Stilt B Soles | 1.4 | 22:35 |
| Day 1 22:50 | g17 Keel B and Stilt B Mounts | 8.2 | Day 2 07:04 |
| Day 2 07:19 | g03 C Bay | 12.1 | 19:25 |
| Day 2 19:40 | g24 g24-asa-C Payload Cover (blank) | 3.1 | 22:44 |
| Day 2 22:59 | g20 C Spar Box | 7.1 | Day 3 06:05 |
| Day 3 07:00 | g23 Clear Light Windows | 0.1 | 07:05 |
| Day 3 07:20 | g18 Keel B and Stilt B Blades and Lids | 8.8 | 16:11 |
| Day 3 17:00 | g09 C Hatch | 4.3 | 21:20 |
| Day 3 21:35 | g14 Seals | 0.8 | 22:20 |
| Day 3 22:35 | g07 Wing Outers (own section) | 6.3 | Day 4 04:55 |
| Day 4 07:00 | g04 C VTOL Section (port) | 6.0 | 12:57 |
| Day 4 17:00 | g12 Plates and Fences | 1.3 | 18:20 |
| Day 4 18:35 | g16 Servo Airspeed Radio Holders and Slider | 3.6 | 22:12 |
| Day 4 22:27 | g05 C VTOL Section (starboard) | 5.9 | Day 5 04:20 |
| Day 5 07:00 | g06 Wing Inners (own section) | 11.9 | 18:56 |
| Day 5 19:11 | g15 C Canopy Beacon Carrier Charge Camera Arm | 3.0 | 22:12 |
| Day 5 22:27 | g10 C Tail Nose Cone Wing Tip B | 4.2 | Day 6 02:42 |
| Day 6 07:00 | g21 C Avionics Q43 Lucid and Aria | 3.0 | 09:59 |
| Day 6 17:00 | g11 Mounts Hardware and Lights | 2.9 | 19:54 |
| Day 6 20:09 | g02 C Front | 12.6 | Day 7 08:48 |
At the same time, the Kobra Max prints g08 Elevons from Day 1 07:00 to 14:36.
The workday plan puts the two longest LW-PLA beds, g02 and g06, in the daytime and the beds of 5 to 8 hours in the night. Thus, the workday plan is less than a day slower than the home all day plan.
Trade-offs
Section titled “Trade-offs”- The assembly manual says to print one part at a time. LW-PLA parts on a grouped bed print together, one layer at a time. Thus, if one part fails or falls over, the adjacent parts can also fail. The travel between parts also causes some stringing with LW-PLA. Monitor the first layers of each grouped bed.
- All parts on a bed use the same settings. We put only parts with identical settings on one bed, except where a part carries its own settings in the project (the M10 Hanger’s pocket supports and the support blockers on the Wing Inners and Wing Outers). The PETG mounts bed (g11) uses 8 bottom layers, for the heat resistance of the pusher mount, and 3 perimeters. These add only a little strength and weight.
- Material changes. The home plan changes material eleven times, between PLA Aero, PETG, TPU and the clear PETG of g23. With the 8-spool kit, these changes cost nothing. Before the 8-spool kit arrives, change the bed order so that beds of one material print one after the other. The total from the optimiser changes only a little.
- The Kobra Max profile is not proven.
slicing/config/printer-kobra-max.iniis our own (PrusaSlicer has no profile for the original Kobra Max). Its 6 mm Bowden retraction and its speeds are starting values. Before g08, run LeviQ from the screen and print the elevon strip test (lw-elevon-strip) and a retraction tower in PLA Aero. - The g01 wing tip controls all other LW-PLA beds. If the test tip is soft, stringy or over-foamed, correct the profile before you start a different bed.
After you change the settings, regenerate with these commands:
uv run --no-project --with trimesh --with numpy --with scipy --with networkx --with rtree \ --with rectpack python tools/slice_all.py --fusCuv run --no-project python tools/plan_schedule.py slicing/summary-fusC.txtSource: docs/print-schedule.md in the repo. Edit it there; this page is generated.
Comments
Comment on the whole page here, or on one section or step with the button beside it.