
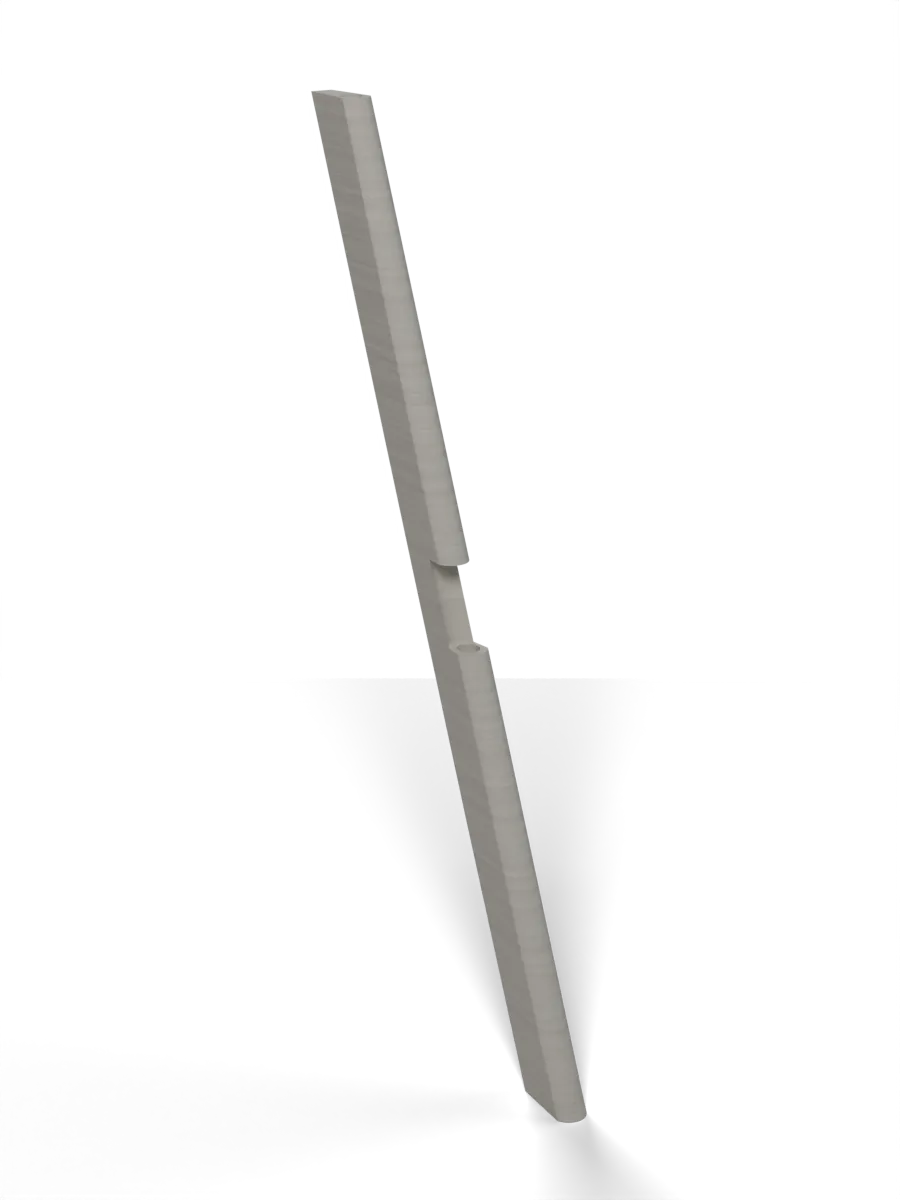
Elevon strip, full height
Test prints / LW-PLA: the foam is the calibration
The elevon's leading edge with its spar bore, full height on the Kobra Max: the riskiest print, for a few grams.
Toolpaths
Every extrusion move in the G-code, layer by layer. Drag the layer slider, scrub through the top layer, or play the print.
Toolpaths load when you open this view.
Read from the G-code that the printer gets. The clock adds each move at its programmed speed, without acceleration or travel, so it is shorter than the slicer's estimate.
Settings
On top of the stack that the print jobs load. The printer tuning page shows that stack.
| Printer | File | Changes |
|---|---|---|
| Anycubic Kobra Max | lw-elevon-strip (kobra-max).gcode | brim_width 12 |
Procedure
What it is for. The elevon, printed in one part, is the riskiest LW-PLA print: a tall single wall on the Kobra Max’s moving bed. This strip prints its leading edge and spar bore at full height, for a few grams, before a full elevon.
Print. Print on the Kobra Max, standing, with the elevon’s 12 mm brim, as the elevon prints. Watch the top third: a tall single wall on a bed-slinger can wobble or break off.
Measure. Check the leading edge for gaps and the layer lines for steps. Push the real 6 mm carbon tube through the full-height bore.
Pass. No gaps, no steps, and the tube passes through the bore. If it does not pass, the elevon will not either.
Record. Pass or fail for each check, and the height where a problem starts.
In the tuning log
Comments
Comment on the whole page here, or on one section or step with the button beside it.