
LW-PLA expansion map
Test prints / LW-PLA: the foam is the calibration
A single-wall coupon at 35 mm/s, 250 down to 200 °C in 10 mm bands: measure and weigh each band.
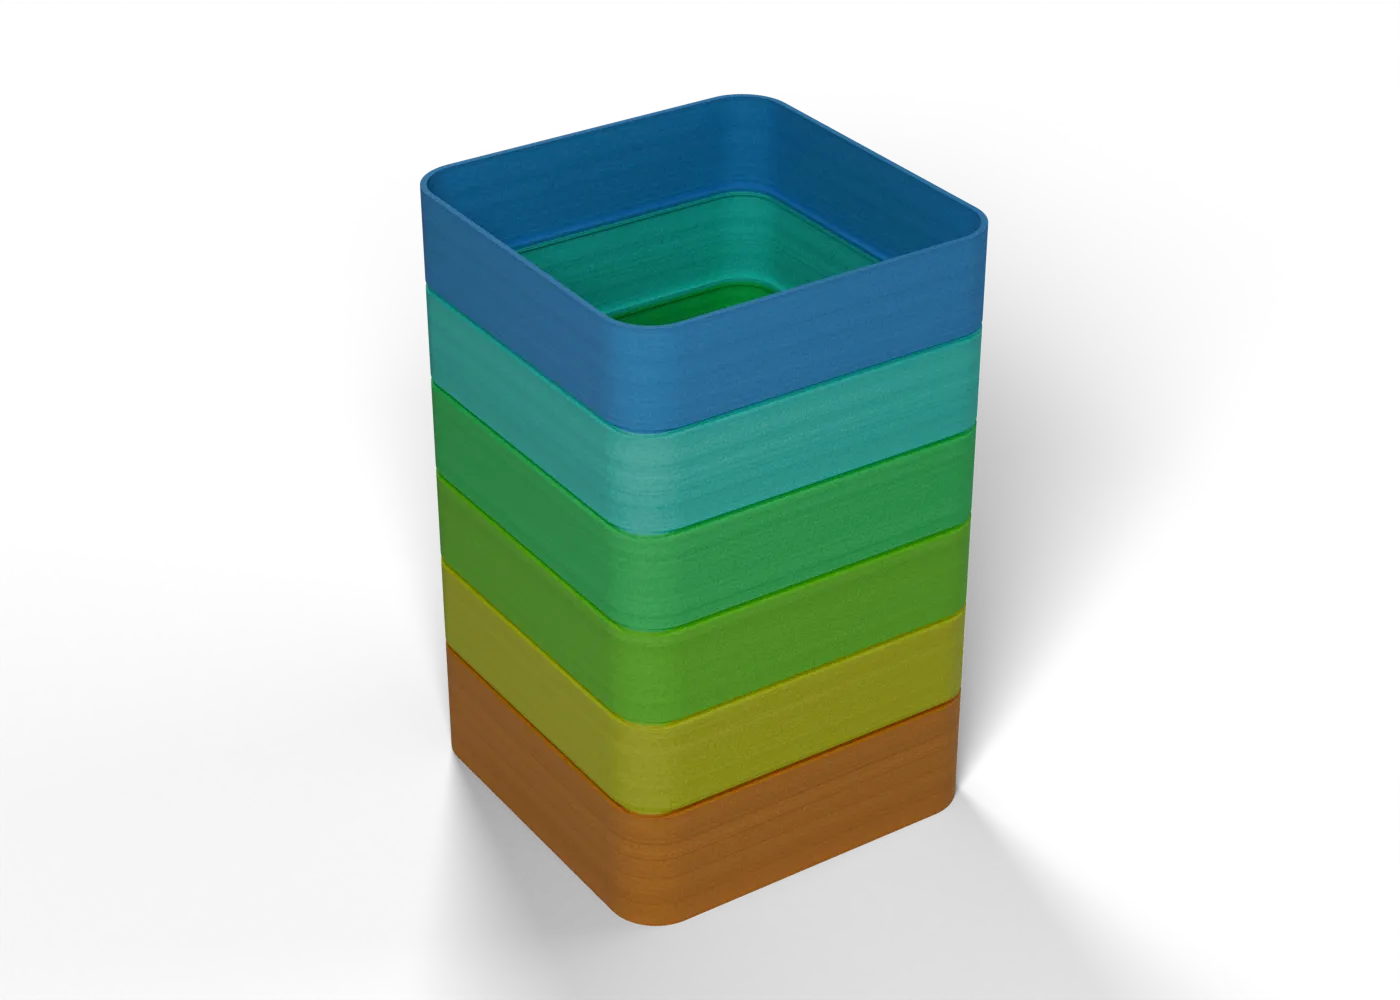
Toolpaths
Every extrusion move in the G-code, layer by layer. Drag the layer slider, scrub through the top layer, or play the print.
Toolpaths load when you open this view.
Read from the G-code that the printer gets. The clock adds each move at its programmed speed, without acceleration or travel, so it is shorter than the slicer's estimate.
Bands
Each band starts with one G-code command on its first layer. The slicing script reads the G-code back and stops if a command is missing or lands at the wrong height.
- 200 °C53–63 mm
M104 S200 - 210 °C43–53 mm
M104 S210 - 220 °C33–43 mm
M104 S220 - 230 °C23–33 mm
M104 S230 - 240 °C13–23 mm
M104 S240 - 250 °C3–13 mm
M104 S250
Base 0–3 mm at the first band's value
Settings
On top of the stack that the print jobs load. The printer tuning page shows that stack.
| Printer | File | Changes |
|---|---|---|
| Prusa Core One+ | lw-expansion (core-one-plus).bgcode | spiral_vase 1support_material 0support_material_auto 0perimeters 1top_solid_layers 0fill_density 0%bottom_solid_layers 3slowdown_below_layer_time 0enable_dynamic_overhang_speeds 0thin_walls 0perimeter_speed 35external_perimeter_speed 35small_perimeter_speed 35temperature 250first_layer_temperature 250 |
| Anycubic Kobra Max | lw-expansion (kobra-max).gcode | spiral_vase 1support_material 0support_material_auto 0perimeters 1top_solid_layers 0fill_density 0%bottom_solid_layers 3slowdown_below_layer_time 0enable_dynamic_overhang_speeds 0thin_walls 0perimeter_speed 35external_perimeter_speed 35small_perimeter_speed 35temperature 250first_layer_temperature 250 |
Procedure
What it is for. LW-PLA foams in the nozzle, and the foam changes with temperature. This test finds the temperature and the flow for every LW-PLA part.
Print. Print one coupon on each printer with the LW-PLA spool you fly. It starts at 250 °C and steps down 10 °C at each groove.
Measure. Let it cool. Turn it over: the underside lists the band temperatures, bottom band first. Then measure the wall at the middle of each band, on all four faces. Cut the bands apart at the grooves with a fine saw and weigh each one to 0.01 g.
Pass. Pick the temperature: the lowest band with a smooth, closed wall and good layer bond (flex it). Then set the flow so the wall at that band equals the extrusion width: new flow = 0.60 × 0.45 / measured wall. The 0.60 at 220 °C is the manual’s value for a Bambu hotend, so expect a difference on the HF0.4 and again on the Kobra Max.
Record. The wall and the mass of each band, the temperature and the new flow. Then ask th-main to put them in the profile.
In the tuning log
- Flow (extrusion multiplier)To test
- Nozzle temperatureTo test
- Nozzle temperature and flowTo test
Comments
Comment on the whole page here, or on one section or step with the button beside it.